


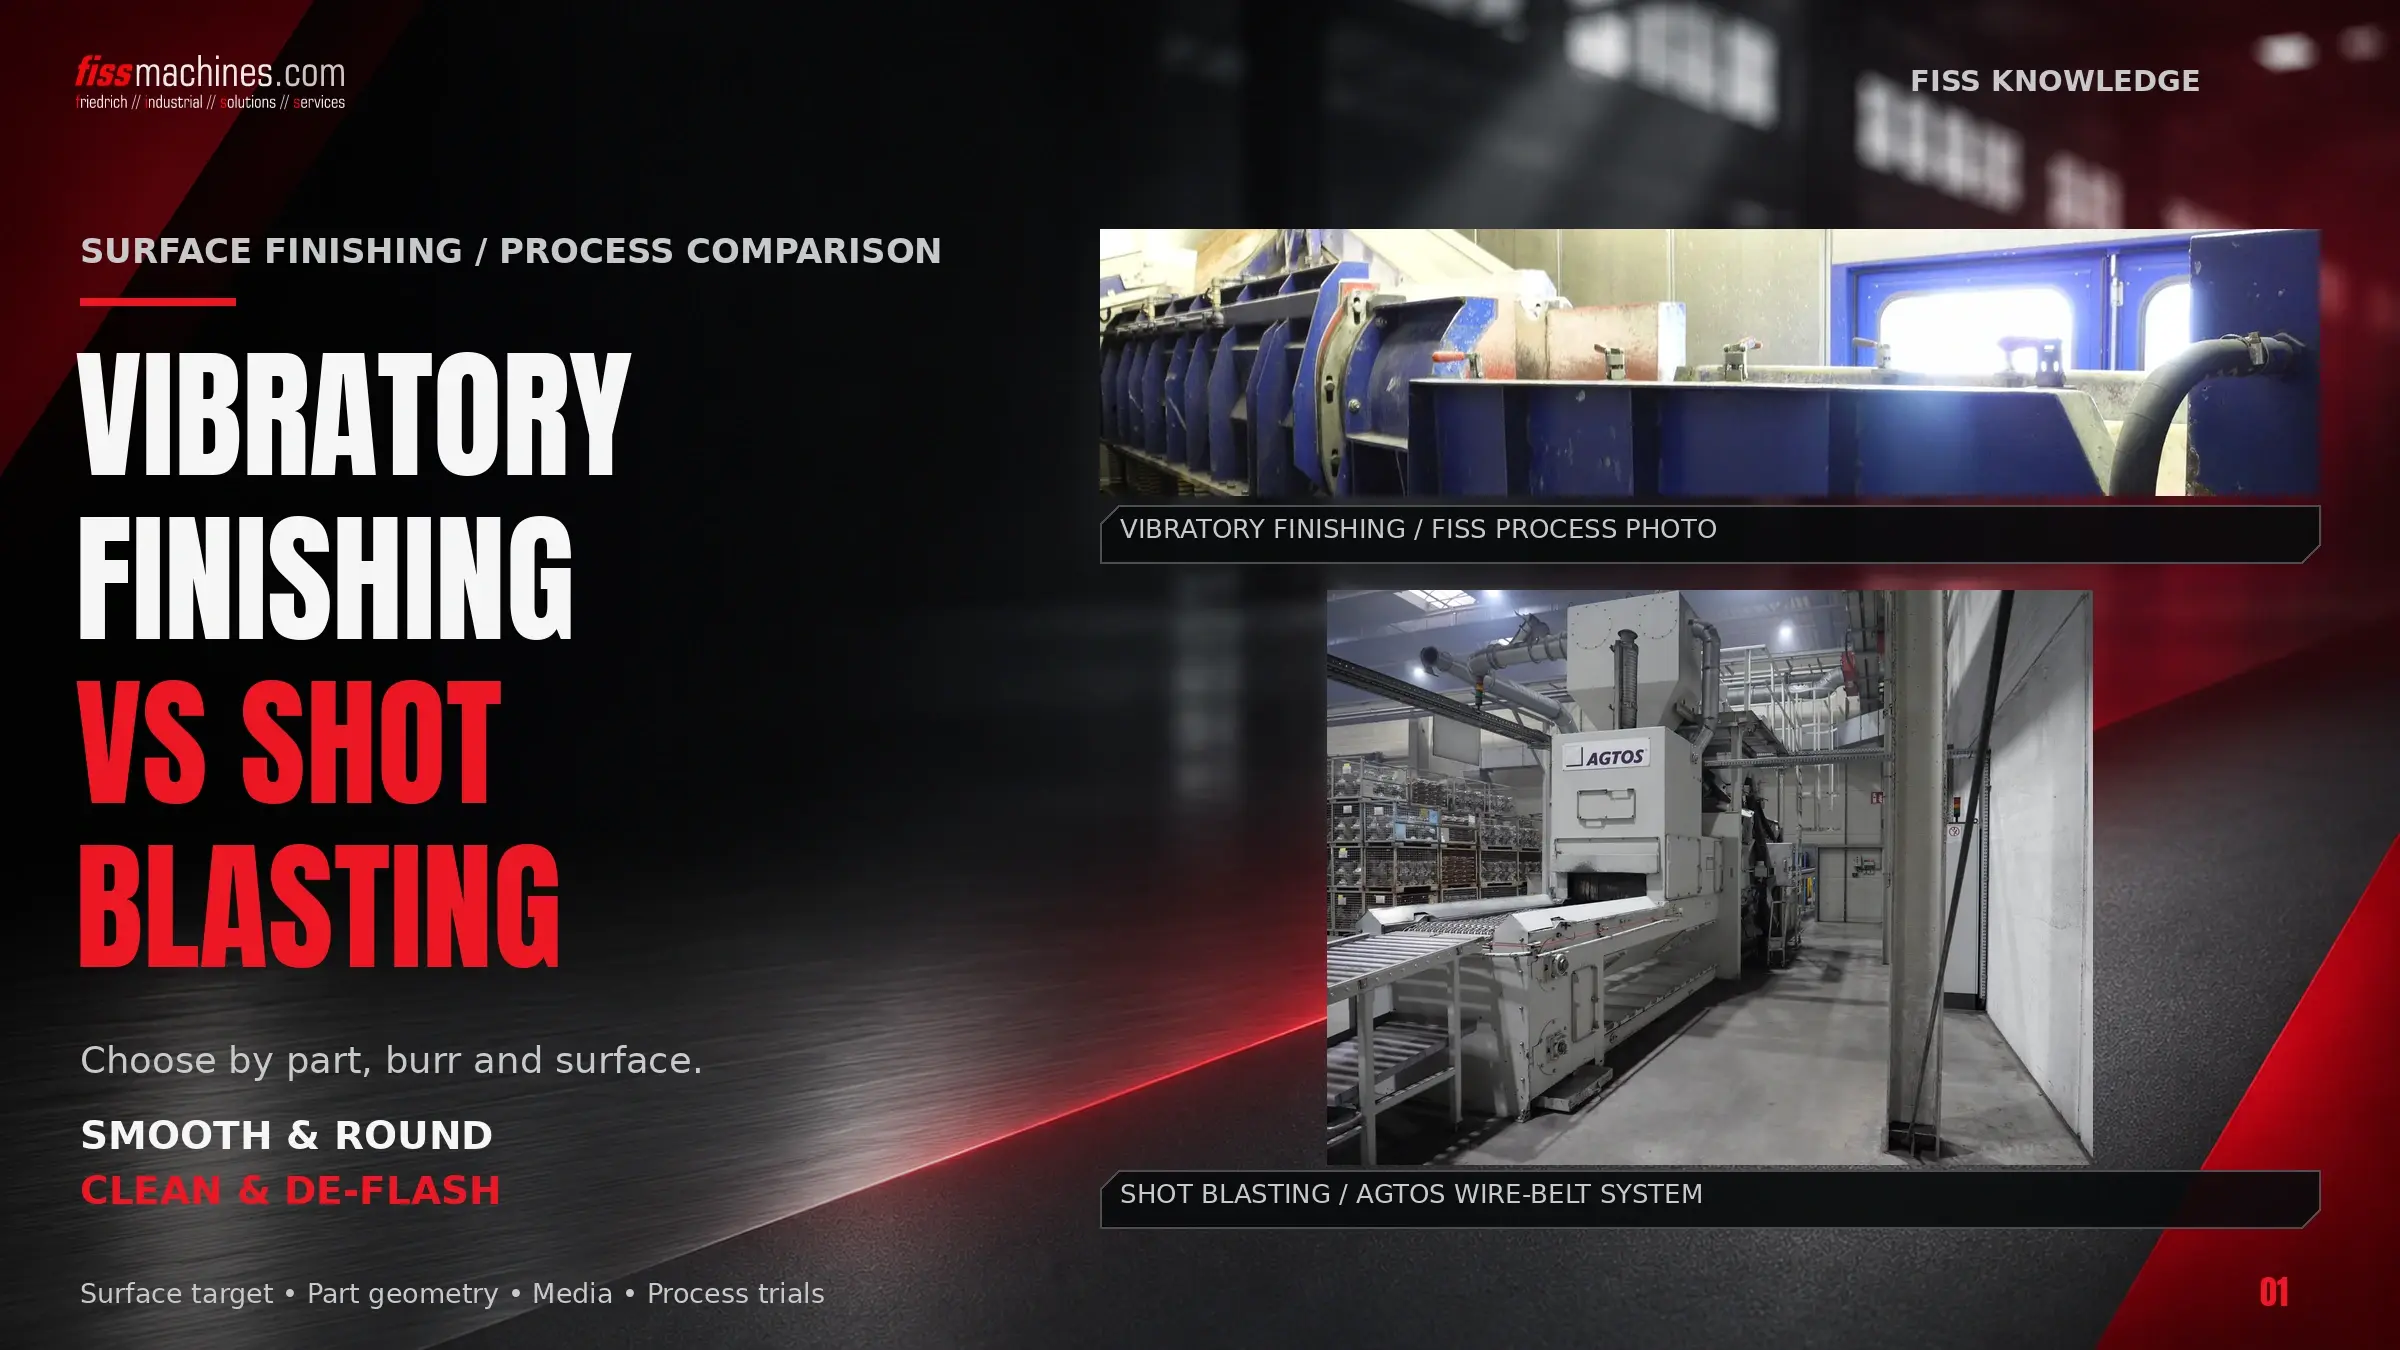
Vibratory Finishing or Shot Blasting? Surface Finishing of Castings Compared
After trimming, most castings still need a finishing step: small burrs and sharp edges have to go, release agent residues and oxides must be removed, and the surface has to meet the customer’s specification. Two processes dominate this step – vibratory finishing and shot blasting. They often solve the same problem, but with different physics, consumables and consequences for the process chain.
Vibratory Finishing vs Shot Blasting: The Short Answer
Vibratory finishing moves parts and abrasive media together in a vibrating bowl or trough, usually wet with water and compound. It is strong at deburring, edge rounding and smoothing and produces even, often bright surfaces. Shot blasting throws blast media at the parts with a turbine wheel or compressed air. It works dry and is strong at cleaning, de-flashing and creating a uniform matt surface.
Which process fits depends on part size and geometry, the required surface, the burr type and the downstream steps. Many die casting plants run both: blasting for larger housings, vibratory finishing for small mass parts.
Two Different Working Principles
Both processes start where trimming ends. How gates and overflows are separated is covered in Trimming in Die Casting; this article deals with the surface work that follows.
Relative Movement in a Mass
Parts and media are set in motion together. The media rub over edges and surfaces and remove burrs; the compound cleans and keeps the media cutting.
Impact of Thrown Media
Blast media hit the surface at high speed and remove flash, residues and scale. The parts stay dry; the result is a uniform, matt surface. A polished finish cannot be achieved by dry blasting.
Vibratory Finishing and Shot Blasting Side by Side
| Criterion | Vibratory Finishing | Shot Blasting |
|---|---|---|
| Process | Usually wet, with water and compound | Dry, with dust extraction |
| Typical tasks | Deburring, edge rounding, smoothing, cleaning, polishing | De-flashing, cleaning, removing sand and scale, matt finish |
| Surface | Smooth to bright, rounded edges | Uniform matt texture |
| Parts | Small to medium mass parts; media must reach the burrs | From small parts to large housings, depending on machine type |
| Consumables | Media, compound, water, energy | Blast media, wear parts, energy, filter elements |
| Auxiliary systems | Process water treatment, rinsing, drying | Media recovery, dust collector, explosion protection where required |
Vibratory Finishing: Media, Compound and Process Water
The result depends less on the machine than on the combination of workpiece, media, compound and process time. Manufacturers such as Rösler and Walther Trowal produce their own media and compounds.
High Cutting Performance
Dense and abrasive; suitable for heavier deburring. Chipping and media lodging in the part must be checked.
Gentler on Soft Alloys
Lighter media for aluminium and zinc where a smooth surface matters more than high removal.
Plastic with Dense Filler
Walther Trowal offers a plastic media filled with zirconium silicate for die castings, with removal rates the manufacturer describes as comparable to ceramic.
The compound is dosed with water; it cleans and keeps media and parts free of fines. The used process water carries metal and media fines. With a centrifuge, solids are separated so that water and compound can be reused several times before final discharge. Where recycling is not possible, the water is treated in a flocculation unit and disposed of.
Shot Blasting: Wheel or Air, and Which Media for Aluminium?
Turbine Throws the Media
A high-speed bladed wheel accelerates the media centrifugally. Efficient for large media quantities and heavy shot; standard in a shot blasting machine for castings.
Compressed Air Carries the Media
Suction or pressure systems accelerate the media in an air stream. Targeted and good for lighter media, but with high compressed air demand.
For aluminium and magnesium castings, the media are chosen so that they de-flash without damaging the part. Aluminium cut wire and stainless steel cut wire are commonly used; AGTOS, for example, states that aluminium is often used as a blast media for light metal castings. The right type and size should be determined in trials with real parts.
Batch or Continuous Machines?
Continuous systems can be linked to the casting and trimming cell and avoid intermediate storage; batch machines are more flexible for changing parts.
| Machine Type | Process | Typical Use |
|---|---|---|
| Rotary vibrator | Vibratory, batch or continuous | Small to medium parts; Walther Trowal also links rotary vibrators directly to the die casting machine |
| Linear continuous trough | Vibratory, continuous | Robust mass parts that need longer processing |
| Centrifugal disc | Vibratory, batch | High-intensity processing of small parts |
| Tumble belt | Blasting, batch | Robust mass castings that may touch each other |
| Troughed belt / wire mesh belt | Blasting, continuous | Linked production; wire mesh belts for sensitive light metal parts |
| Spinner hanger | Blasting, batch or continuous | Larger housings that must not collide |
Manufacturer examples show the range: Walther Trowal states cycle times of around four minutes for light deburring of die castings in its CB 400 rotary vibrator, and specifies its compact THM, a continuous shot blasting machine with troughed belt, for aluminium and zinc die castings of 20 to 150 mm diagonal. Rösler has installed a continuous spinner hanger machine with aluminium cut wire for distortion-sensitive aluminium housings.
Typical Process Chains in Practice
Two illustrative chains show how the choice depends on the part:
Small Zinc Fittings, Decorative Surface
Trimming press, then continuous vibratory finishing with plastic media, rinsing and drying, then plating.
Aluminium Housing with Sealing Faces
Trimming, then blasting on a spinner hanger with aluminium cut wire, washing and CNC machining. Parts hang separately; sealing faces are masked or machined later.
Checklist: Which Process Fits Your Castings?
- Which burrs remain after trimming – thin flash or firm residues?
- Which surface does the drawing or customer require: rounded, smooth, bright or uniformly matt?
- Size, weight, wall thickness: may parts touch each other, or must they hang separately?
- Do media reach all edges, and can they lodge in bores or pockets?
- Is the part allowed to get wet, and are rinsing, drying and water treatment available?
- Batch or continuous: is the line linked to the casting cell?
For a used machine, wear parts, lining, safety documentation and complete auxiliary units (centrifuge, dryer, dust collector) count as much as the basic machine. FISS lists used vibratory finishing machines, centrifuges and dryers as well as shot blasting machines, for example from Rösler, Walther Trowal and AGTOS.
Choose by Part and Surface, Not by Machine
Vibratory finishing is the stronger process for deburring, edge rounding and smooth surfaces on small and medium mass parts – at the price of a wet process with water treatment and drying. Shot blasting cleans and de-flashes dry, also handles large housings and produces a uniform matt finish, but requires suitable media, dust extraction and, for light metals, a careful protection concept.
Questions About Vibratory Finishing and Shot Blasting
Can Vibratory Finishing Replace Trimming?
No. Vibratory finishing removes small residual burrs and sharp edges. Gates, overflows and larger flash are separated beforehand by trimming or machining.
Which Blast Media Are Used for Aluminium Die Castings?
Aluminium cut wire and stainless steel cut wire are common. Type and size depend on the burr, the required surface and the part sensitivity and should be tested on real parts.
Why Does a Vibratory Finishing Line Need a Centrifuge?
The centrifuge separates metal and media fines from the process water so that water and compound can be reused. This reduces consumption and the amount of wastewater.
Are Continuous Machines Always Better?
Not always. They suit linked, high-volume production. With frequently changing parts and small batches, batch machines are often more flexible.
Used Shot Blasting and Vibratory Finishing Machines from FISS.
FISS lists used shot blasting machines and vibratory finishing equipment from established manufacturers. Tell us your parts and requirements – we will help you find a suitable machine.
Sources
Foundry Trade Journal / Rösler: Surface finishing options for diecasters, foundrytradejournal.com, accessed 5 November 2026.
Walther Trowal: press release Rotary solutions for castings and stampings save time, space and costs, 9 October 2020; and For the first time Walther Trowal displays shot blast machinery at the show, 18 August 2022, presseportal.org, accessed 5 November 2026.
Foundry Management & Technology: New Plastic Grinding Media for Diecastings (Walther Trowal HDC), 15 March 2016, accessed 5 November 2026.
EUROGUSS 365: Automated all-round solution for low-distortion blasting processes (Rösler / Alupress), 2025, euroguss.de, accessed 5 November 2026.
Foundry Trade Journal / AGTOS: Efficient surface technology – optimum shot blast technology for castings, foundrytradejournal.com, accessed 5 November 2026.
Total Materia: Abrasive Blast Cleaning: Part Three (wheel and air blasting), totalmateria.com, accessed 5 November 2026.
IFA / DGUV: research project BGIA 3111 Explosion hazards during the blasting of metals, completed 2009, dguv.de, accessed 5 November 2026.
FISS Machines: categories Vibratory Finishing Machines and Shot Blasting Machines, fiss-machines.com, accessed 5 November 2026.
